+91 73059 50939
Loading...
Loading, please wait...

One Stop Solution
Available for Quote
Worldwide Delivery
We deliver products globally
Support 24/7
Reach our experts today!
First Purchase Discount
Up to 5% discount
Easy Returns
Read our return policy
Product Details
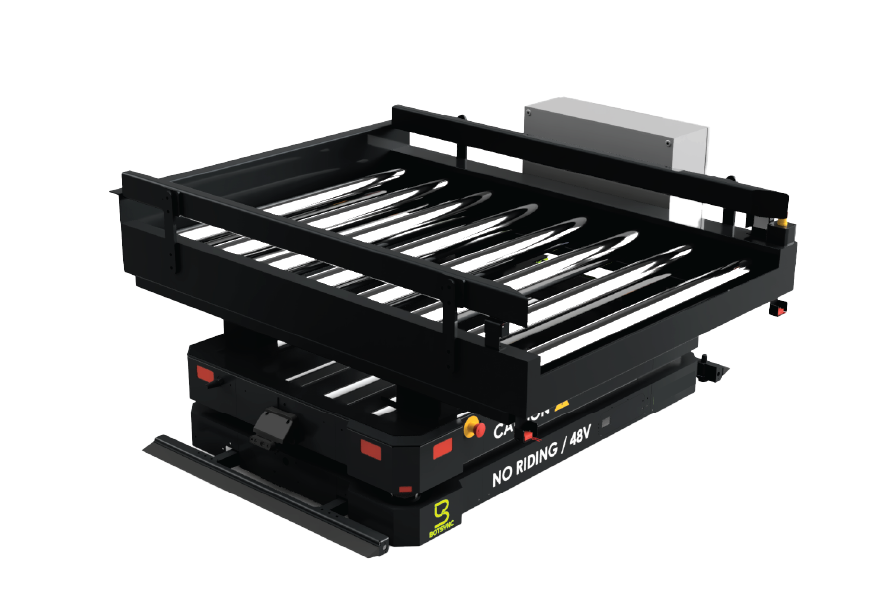
The AMR with Single Conveyor is an advanced autonomous mobile robot designed to automate material movement between conveyor lines, production workstations, and automated storage systems. Equipped with an integrated conveyor top, it enables smooth, hands-free transfer of cartons, totes, and packaged goods while reducing manual handling and increasing operational efficiency.
Designed for modern warehouses and manufacturing facilities, this conveyor AMR supports payloads of up to 1,500 kg and delivers reliable autonomous navigation using intelligent sensors, LiDAR-based localization, and real-time obstacle detection. Its seamless integration with existing conveyor systems helps optimize production flow, minimize downtime, and improve workplace safety.
Ideal for distribution centers, e-commerce fulfillment, automotive, FMCG, food processing, and industrial manufacturing, the AMR with a single conveyor provides a scalable and efficient solution for automated material handling.
Autonomous Mobile Robot (AMR) with integrated single conveyor.
Supports payload capacity up to 1,500 kg.
Seamless transfer between conveyor lines and automated storage systems.
Intelligent LiDAR-based navigation with real-time obstacle avoidance.
High-precision docking for conveyor integration.
Self-navigation without fixed tracks or guide paths.
Operating speed up to 1.4 m/s.
Long battery runtime of 9–10 hours.
Fast charging in approximately 2 hours.
Compatible with warehouse management and factory automation systems.
Reduces manual material handling and improves productivity.
Suitable for warehouses, manufacturing plants, distribution centers, and logistics operations.
Specifications
An AMR with a single conveyor is an autonomous mobile robot equipped with an integrated conveyor that automatically transfers materials between conveyor lines, workstations, and storage systems. The robot can handle loads of up to 1,500 kg, making it suitable for heavy-duty industrial material handling. It is ideal for warehouses, manufacturing plants, automotive industries, FMCG, logistics, e-commerce fulfillment centers, and distribution hubs. No. It uses autonomous navigation with LiDAR and intelligent sensors, allowing flexible movement without fixed guide paths. Yes. The AMR is designed for seamless integration with conveyor lines, automated storage systems, and production workflows. The robot provides approximately 9–10 hours of continuous operation and can be fully recharged in around 2 hours. It incorporates LiDAR sensors, intelligent obstacle detection, emergency stop functionality, safety-rated navigation, and precision docking to ensure safe operation in dynamic environments. A conveyor AMR automates repetitive material transport, reduces labor dependency, improves workflow efficiency, minimizes handling errors, enhances safety, and supports scalable warehouse automation.Frequently Asked Questions (FAQs)
1. What is an AMR with a single conveyor?
2. What is the payload capacity?
3. What industries can use this conveyor AMR?
4. Does the robot require fixed tracks?
5. Can it integrate with existing conveyor systems?
6. How long does the battery last?
7. What safety features are included?
8. What are the advantages of using a conveyor AMR?
The AMR with Single Conveyor is an advanced autonomous mobile robot designed to automate material movement between conveyor lines, production workstations, and automated storage systems. Equipped with an integrated conveyor top, it enables smooth, hands-free transfer of cartons, totes, and packaged goods while reducing manual handling and increasing operational efficiency.
Designed for modern warehouses and manufacturing facilities, this conveyor AMR supports payloads of up to 1,500 kg and delivers reliable autonomous navigation using intelligent sensors, LiDAR-based localization, and real-time obstacle detection. Its seamless integration with existing conveyor systems helps optimize production flow, minimize downtime, and improve workplace safety.
Ideal for distribution centers, e-commerce fulfillment, automotive, FMCG, food processing, and industrial manufacturing, the AMR with a single conveyor provides a scalable and efficient solution for automated material handling.
Autonomous Mobile Robot (AMR) with integrated single conveyor.
Supports payload capacity up to 1,500 kg.
Seamless transfer between conveyor lines and automated storage systems.
Intelligent LiDAR-based navigation with real-time obstacle avoidance.
High-precision docking for conveyor integration.
Self-navigation without fixed tracks or guide paths.
Operating speed up to 1.4 m/s.
Long battery runtime of 9–10 hours.
Fast charging in approximately 2 hours.
Compatible with warehouse management and factory automation systems.
Reduces manual material handling and improves productivity.
Suitable for warehouses, manufacturing plants, distribution centers, and logistics operations.
Specifications
An AMR with a single conveyor is an autonomous mobile robot equipped with an integrated conveyor that automatically transfers materials between conveyor lines, workstations, and storage systems. The robot can handle loads of up to 1,500 kg, making it suitable for heavy-duty industrial material handling. It is ideal for warehouses, manufacturing plants, automotive industries, FMCG, logistics, e-commerce fulfillment centers, and distribution hubs. No. It uses autonomous navigation with LiDAR and intelligent sensors, allowing flexible movement without fixed guide paths. Yes. The AMR is designed for seamless integration with conveyor lines, automated storage systems, and production workflows. The robot provides approximately 9–10 hours of continuous operation and can be fully recharged in around 2 hours. It incorporates LiDAR sensors, intelligent obstacle detection, emergency stop functionality, safety-rated navigation, and precision docking to ensure safe operation in dynamic environments. A conveyor AMR automates repetitive material transport, reduces labor dependency, improves workflow efficiency, minimizes handling errors, enhances safety, and supports scalable warehouse automation.Frequently Asked Questions (FAQs)
1. What is an AMR with a single conveyor?
2. What is the payload capacity?
3. What industries can use this conveyor AMR?
4. Does the robot require fixed tracks?
5. Can it integrate with existing conveyor systems?
6. How long does the battery last?
7. What safety features are included?
8. What are the advantages of using a conveyor AMR?


 Start Chat